Hey, let’s cut to the chase – if you’re in water treatment, biomanufacturing, food & beverage, or even pharma, you’ve probably heard someone mumble “membrane filtration equipment” at some point, but maybe you’re still like, “Wait, is that just fancy lab filters?” Spoiler: it’s way more, and if you’re picking gear for your operation, getting this right can save you thousands in downtime or even regulatory headaches down the line. As a membrane filtration equipment supplier, I don’t just sell parts – I’ve spent years troubleshooting these systems for small breweries and big municipal plants alike, so let’s break this down like I would over a coffee with a client. Membrane Filtration Equipment
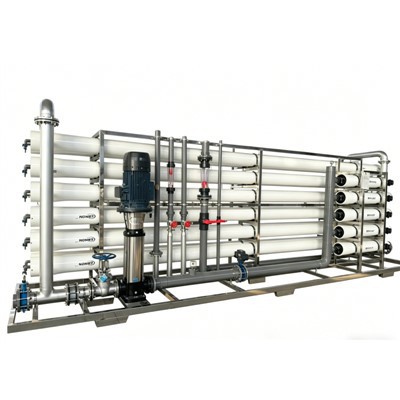
First, let’s define the basics without boring you with 101 textbook jargon. Membrane filtration equipment is basically a system that uses thin, porous membranes (think super tiny sails, but holes so small they can catch bacteria, microplastics, or even dissolved solids) to separate, purify, or concentrate substances from a liquid or gas. The key here is the membrane’s pore size – that’s what differentiates one type from another, and it’s not one-size-fits-all. You can’t use a membrane meant for drinking water to sterilize biotech cell culture, for example; that’s how mistakes happen.
Let’s walk through the main types because this is where people get confused, and I see mix-ups all the time. Microfiltration (MF) is the big, “course” one – pores are 0.1 to 10 micrometers. That’s perfect for catching big stuff like bacteria, yeast, or sediment. We’ve sold MF systems to craft breweries that want to clear their beer without using harsh fining agents, and to small municipalities polishing surface water before it goes to a reverse osmosis (RO) system. Then there’s Ultrafiltration (UF), pores between 0.001 and 0.1 micrometers. This can catch viruses, proteins, and even some larger dissolved molecules – biotech firms use UF all the time to concentrate monoclonal antibodies (mAbs) without damaging them, and dairy companies use it to separate whey proteins from milk for protein powders.
Next, Nanofiltration (NF) – this is the middle child, pores around 0.001 micrometers. It’s great for removing hardness minerals (calcium, magnesium) from water, or concentrating dyes and sugars in food processing. It’s less expensive than RO, so a lot of factories use it as a middle step to cut down on RO energy costs. Then there’s Reverse Osmosis (RO), the one you’ve definitely heard of. Pores are tiny – like 0.0001 micrometers – so they can filter almost everything, including dissolved salts, heavy metals, and even some small molecules. RO systems are used for desalination, high-purity water for labs, and tap water for homes, but they’re super energy-heavy, so you can’t just swap an RO for a UF and call it a day.
Now, how does the actual equipment work? It’s not just slapping a membrane in a box. Most systems use one of two setups: cross-flow (tangential) flow or dead-end flow. Dead-end flow is simpler – liquid is pushed straight through the membrane, and all the stuff that gets caught stays on the surface. But the problem is that gunk builds up fast, so you have to clean it constantly, which is a pain for high-volume operations. Cross-flow is the workhorse – liquid is pushed parallel to the membrane, so the part that doesn’t go through (the “retentate”) sweeps away the gunk as it flows. That means less fouling, longer membrane life, and you can run it 24/7 if you need to. I’ve had clients who switched from dead-end to cross-flow and cut their cleaning time by 70% – that’s not just a number, that’s more time for their plant to make money.
Wait, but what makes a good membrane filtration system, not just a cheap one? A lot of cut-rate suppliers will sell you a bare-bones system, but the hidden costs add up fast. First, membrane material matters. Polyethersulfone (PES) is super common and works for most water and biotech uses, but if you’re dealing with harsh chemicals (like strong acids or solvents), you need something like polytetrafluoroethylene (PTFE) – those membranes don’t break down. Second, the system’s pre-treatment step is non-negotiable. If you feed sediment or big gunk into a membrane, it’ll clog in a week, not a year. I can’t tell you how many times I’ve had a brand new system down because the client skipped the $50 pre-filter that would have saved their $5,000 membrane. Third, automation – small operations can get away with manual cleaning, but if you’re running 100,000 gallons a day, automated CIP (clean-in-place) systems are a must. They save labor, reduce human error, and keep membranes working consistently.
Now, let’s talk about where people mess up when choosing membrane equipment. I get calls all the time from guys who say, “I need a system for 5,000 gallons a day – give me the cheapest one.” But they don’t tell me they’re dealing with 5,000 gallons of raw wastewater with 10% suspended solids, so a cheap MF system will foul before it hits 2,000 gallons. Another common mistake: sizing wrong. If you size a system for peak demand but run it at half capacity all the time, that’s also a recipe for fouling. Membranes work best when they’re operated within their design flow rate, so you have to account for future growth too – don’t buy a system that’ll be too small in 2 years when your brewery expands.
As a supplier, my job isn’t just to drop a system off and leave. I’ve had clients call me at 2 a.m. when their membrane pressure spikes, and I can walk them through a quick flush to fix it before the whole line shuts down. We also offer regular maintenance checks, membrane replacement schedules tailored to their use, and even help with compliance – like if you’re in pharma, we make sure our systems meet FDA standards, so you don’t get hit with a warning letter. That’s the stuff you don’t see when you look at a price tag, but it’s what makes working with the right supplier worth it.
Let’s wrap this up: membrane filtration equipment isn’t a “set it and forget it” gadget, it’s a specialized tool that needs to match your specific application. Whether you’re purifying water, concentrating biotech products, processing food, or treating industrial wastewater, the pore size, flow type, membrane material, and pre-treatment are all make-or-break factors. Cut corners, and you’ll end up with higher operating costs, more downtime, and even product issues. Do it right, and it’ll pay for itself in a year or two.
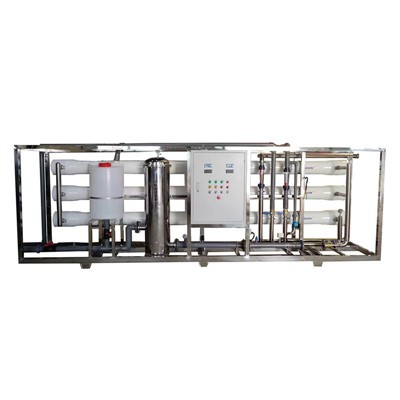
If you’re shopping for a membrane filtration system, don’t just go for the lowest quote. Reach out, tell me what you’re working on, how much volume you need, what you’re filtering, and any specific requirements you have. I can help you avoid the mistakes that almost every new client makes, and build a system that works for your long-term goals, not just your immediate budget. I’m here to help, not just sell – that’s why so many of my clients come back when they need to expand or switch processes.
Reverse Osmosis Water System References:
- Baker, R.W. (2012). Membrane Technology and Applications. John Wiley & Sons.
- Li, N. N., Fane, A. G., & Winston Ho, W. S. (Eds.). (2011). Membrane Handbook (2nd ed.). CRC Press.
- Water Environment Federation. (2019). Membrane Filtration for Water and Wastewater Treatment. WEF Press.
- Côté, P., & Ampudia, F. (2020). Ultrafiltration and Microfiltration for Food and Beverage Processing. Elsevier.
- U.S. Food and Drug Administration. (2021). Guidance for Industry: Membrane-Based Processes for Biologic Products. FDA.
Shandong Yanuo Environmental Protection Equipment Co., Ltd.
We’re well-known as one of the leading membrane filtration equipment manufacturers and suppliers in China, featured by quality products and good price. Please rest assured to buy bulk membrane filtration equipment made in China here from our factory. Customized orders are welcome.
Address: North Side of the Road, 1,000 Meters West of the Intersection of Fenghuangshan West Road and Provincial Highway S102, Wangfu Subdistrict, Qingzhou City, Weifang City, Shandong Province.
E-mail: ynhb.499973983@gmail.com
WebSite: https://www.zkyaruo.com/
